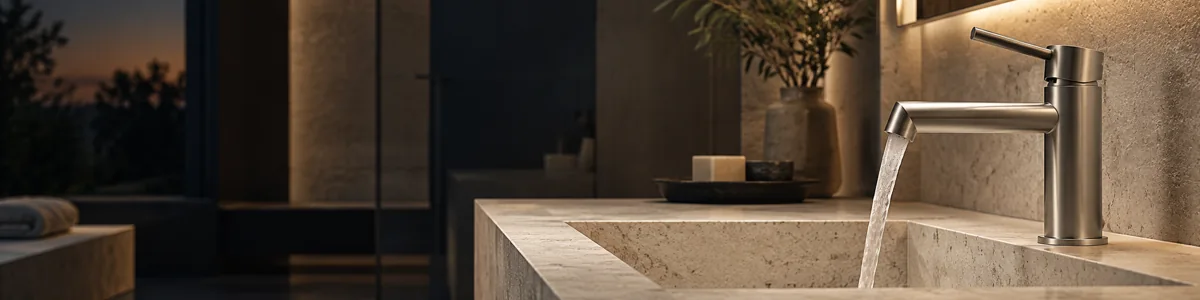
Yes, but not for the reason most spec writers assume. The profile itself, minimalist or traditional, is not what ASME A112.18.1 cares about. What changes lead time and approval risk is the cartridge and body architecture that the profile forces, and how many stocked substitutes exist at that price point. A low-profile single-hole lavatory faucet with a concealed cartridge can add two to four weeks over a traditional widespread with a compression valve, purely on sourcing.
Why Profile Drives Cartridge Complexity
Every faucet submittal eventually reduces to two questions: what valve is inside, and what connects it to the supply. Traditional cross-handle or lever faucets have historically used compression valves or simple quarter-turn ceramic cartridges housed in a body with room to spare. Minimalist single-lever or wall-mount profiles compress that same cartridge into a smaller bore, often requiring a proprietary cartridge shaped to the manufacturer’s own body casting. That proprietary fit is the submittal risk. A compression valve is dumb but replaceable from a dozen suppliers. A custom ceramic disc cartridge built for a specific slim-body faucet may come from exactly one factory.
This matters at the schedule level because a substitution request on a custom cartridge faucet is not a swap of equal parts. It is a redesign of the rough-in, sometimes the wall cavity, if the replacement body has different depth or centerset dimensions.
Minimalist Geometries and Custom Lead Times
Low-profile and wall-mounted minimalist faucets typically use ceramic disc cartridges with tight tolerances, because there is no room inside the body for a traditional stem and packing. These cartridges are manufactured to match the specific casting, which means they are rarely interchangeable across brands even when the exterior finish and handle style look similar in a cut sheet photo.
Three lead time drivers show up repeatedly on minimalist specs:
- Custom cartridge fabrication tied to a single body casting, with no generic stock equivalent.
- Reduced supply thread clearance, sometimes requiring a manufacturer-specific adapter rather than standard 1/2″ NPSM.
- Finish runs tied to minimum order quantities, since slim-body faucets sell in lower volume than standard widespreads.
None of this is a defect in the design. It is simply a smaller supply chain for a smaller category of part, and the spec should account for it with lead time language rather than hoping the GC catches it during submittal review.
Traditional Fixtures and Stocked Substitutions
Traditional profiles, three-hole widespreads, cross handles, exposed bridge faucets, tend to use either compression valves or oversized ceramic disc cartridges that have been standardized across multiple manufacturers for decades. This is why traditional fixtures generate more substitution requests but fewer schedule delays: the contractor has options. If the specified compression valve faucet is back ordered, there is usually a comparable unit from another manufacturer using the same thread pitch and a similar stem depth.
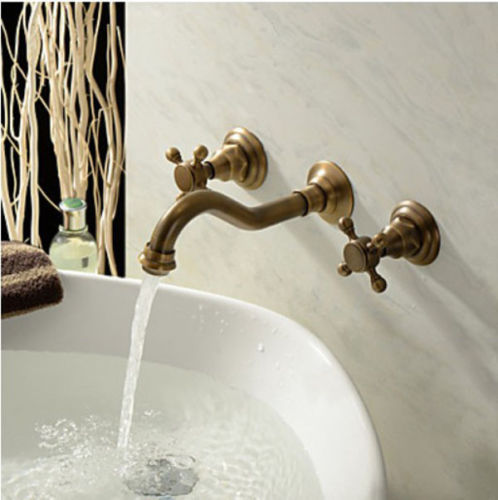
For strictly traditional, period-correct work, such as antique brass basin sets specified for a restoration or a heritage-styled renovation, the supply chain is narrower than standard contemporary widespreads but still more substitutable than a proprietary minimalist cartridge, since compression-valve internals are largely generic across vendors. A specifier pulling from a catalog of period style faucets should still confirm cartridge type on the cut sheet rather than assuming “traditional” implies “generic internals,” because some manufacturers now put ceramic disc cartridges inside traditional-looking bodies purely for warranty reasons.
The practical upshot: traditional does not mean low-risk by default. It means check the cartridge line on the cut sheet before assuming substitution flexibility.
Reading Cut Sheets for Hidden Delays
Cut sheets rarely say “custom cartridge, six to eight week lead time” in plain language. The information is there, but encoded. Below is what to check before you lock a line item into the fixture schedule.
| Cut sheet field | What it tells you | Why it matters for schedule |
|---|---|---|
| Valve type (compression vs ceramic disc) | Internal mechanism and wear profile | Ceramic disc in a proprietary body limits substitution options |
| Supply connection thread | Usually 1/2″ NPSM, sometimes NPT or proprietary | Non-standard thread forces an adapter order or rough-in change |
| Flow rate (GPM) | Typically 1.5 to 2.2 GPM for lavatory faucets | Confirms ASME A112.18.1 and state code compliance before submittal, not after |
| Body depth / rough-in dimension | Physical clearance behind the wall or deck | Minimalist bodies sometimes need shallower or deeper rough-in than standard |
| Finish MOQ note (if listed) | Minimum order quantity per finish run | Small projects may wait for a batch run on uncommon finishes |
The GPM range matters beyond water conservation. A faucet spec’d at 1.5 GPM for a California project and 2.2 GPM for one outside it is not interchangeable without a compliance note, and the plan reviewer will flag it if the cut sheet and the fixture schedule disagree on flow rate. Catching this at submittal avoids a resubmittal cycle that has nothing to do with the faucet’s mechanical performance and everything to do with a clerical mismatch between documents.
Writing Specs That Resist Value Engineering
A fixture schedule that just names a model number invites value engineering substitutions that look identical on paper but introduce cartridge or thread mismatches in the field. Three lines of added language close most of that gap:
- State the cartridge type explicitly (ceramic disc or compression) rather than relying on the model number to imply it.
- Specify the supply thread as 1/2″ NPSM unless the rough-in is already built around something else, and flag any deviation in red on the schedule.
- Include the GPM figure in the schedule itself, not just the cut sheet, so a substitution request that changes flow rate is caught by the reviewer instead of the plumber.
This level of detail costs a few extra minutes per line item and saves a resubmittal cycle that can run two to three weeks depending on the review board’s schedule. On a minimalist spec where the cartridge is already proprietary, that extra language is the only thing standing between an approved submittal and a contractor substitution that technically meets code but does not fit the rough-in.
Before issuing the final fixture schedule, confirm three things directly from the manufacturer rather than the distributor rep: current cartridge lead time, confirmed thread type at the supply connection, and whether the GPM listed on the current cut sheet matches the version actually in production. Cut sheets lag behind running changes more often than anyone likes to admit, and a five-minute phone call is cheaper than a rejected submittal three weeks before rough-in inspection.